Inquiry
Form loading...
Global buyers are entering 2026 with stricter expectations for consistency, safety, and documented performance. Smoke Stabilization is becoming an important consideration in food, beverage, and other regulated manufacturing applications. It helps producers manage smoke-derived aroma, color, and flavor during processing and storage. However, the right solution depends on the product, equipment, climate, and target market.
Experienced suppliers usually begin with the production problem, not a standard catalogue formula. A beverage plant may need a clean smoky note that survives pasteurization. A food processor may require stable color after transport through hot, humid regions. These situations demand different carriers, concentrations, and testing methods. Laboratory trials can reveal changes in aroma, sediment, pH, and packaging compatibility.
Reliable purchasing also requires clear technical evidence. Buyers should request specifications, safety data, certificates of analysis, allergen information, and batch traceability. Production samples matter more than polished sales language. Ask how the material performs after repeated temperature changes. Ask whether the supplier can support consistent batches.
Regulatory requirements also vary across destinations. A formulation accepted in one market may need additional review elsewhere. Suppliers should provide accurate documentation without promising universal approval. That promise is rarely realistic.
Small details matter.
This guide examines practical Smoke Stabilization solutions for global buyers. It considers application fit, supplier capability, storage conditions, and quality control. It also recognizes an uncomfortable truth: no single system works perfectly everywhere. Some recommendations may require further testing. That is not a weakness. It is responsible procurement.
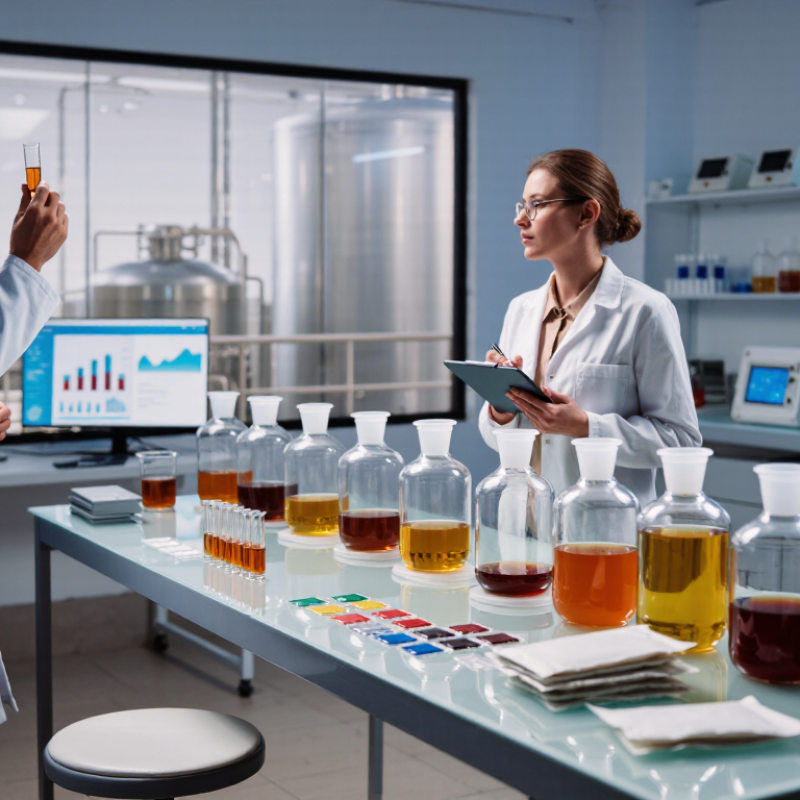
Smoke stabilization is the controlled process of keeping smoke-derived color, aroma, and flavor consistent in food products. It may involve purified smoke compounds, controlled application, oxygen management, and suitable packaging. The goal is not simply a darker surface. A stable result should remain recognizable after processing, transport, storage, and cooking. In practical testing, buyers compare samples after heat exposure and several weeks of storage.
Global buyers need this control because supply chains rarely offer identical conditions. A product may leave a humid factory, cross a cold route, and reach a warm warehouse. Light, oxygen, moisture, and temperature can change smoke color or create uneven flavor. Stabilization reduces these variations and supports repeatable specifications across markets. It also helps technical teams document dosage, application time, packaging barriers, and shelf-life performance. That documentation matters when multiple factories produce the same item.
Reliable evaluation requires more than a promising first sample. Buyers should request batch records, migration data where relevant, sensory results, and accelerated stability evidence. They should also test the finished product, not only the smoke ingredient. Small differences in fat, salt, surface moisture, or cooking temperature can change performance. I have found that simple pilot trials often reveal problems hidden by laboratory conditions. No method is perfect. A stable formula can still fail when packaging or processing changes. That weakness deserves honest review before large-volume purchasing.
| Solution Category | How It Stabilizes Smoke Characteristics | Typical Food Applications | Relevant Technical Parameters | Main Benefits | Key Limitations | Global Buyer Suitability |
|---|---|---|---|---|---|---|
| Purified Liquid Smoke | Smoke is generated, condensed, and refined to remove a substantial portion of ash, tar, and unwanted particulate matter before controlled application. | Processed meat, poultry, seafood, cheese, plant-based proteins, sauces, marinades, and snack seasonings. | Application dosage, pH, density, color intensity, phenolic content, carbonyl content, and microbiological specifications. | Consistent flavor, easier dosing, reduced smokehouse variability, and lower direct exposure to combustion emissions. | May require formulation trials because flavor intensity and color can vary with concentration and food matrix. | High suitability for export products requiring repeatable sensory performance and batch-to-batch control. |
| Controlled Natural Smoking | Temperature, humidity, airflow, smoke density, residence time, and product exposure are monitored to reduce process fluctuations. | Ham, bacon, sausages, fish, poultry, cheese, and traditional smoked specialty foods. | Smoking temperature, relative humidity, air velocity, smoke density, exposure time, product surface temperature, and weight loss. | Preserves traditional processing characteristics while improving color, flavor, and production repeatability. | Higher equipment, monitoring, ventilation, cleaning, and operator-control requirements than liquid application. | Suitable for buyers seeking an authentic smoke process and products positioned around traditional production. |
| Electrostatic Smoke Application | An electrical field helps direct charged smoke particles toward the product surface, improving deposition efficiency and uniformity. | Meat, poultry, seafood, cheese, and products requiring rapid surface smoke deposition. | Voltage, electrode distance, conveyor speed, smoke concentration, surface moisture, and product geometry. | Shorter smoking time, improved surface coverage, and potentially lower smoke consumption when correctly calibrated. | Requires specialized electrical equipment, safety controls, grounding, and validation for different product shapes. | Best for medium- to large-scale processors with established maintenance and process-control capabilities. |
| Smoke Condensate and Filtration | Condensation and filtration separate smoke components according to volatility, solubility, and particle size, helping reduce tar, ash, and unstable solids. | Liquid smoke ingredients, food coatings, seasoning systems, sauces, and industrial smoke-generation systems. | Condensation temperature, filtration grade, solids content, turbidity, phenolic profile, and storage stability. | Improves clarity, dosing consistency, storage stability, and control of unwanted particulate material. | Processing conditions can alter flavor balance; filtration systems require cleaning and periodic maintenance. | Suitable for ingredient manufacturers and buyers requiring documented composition and controlled product quality. |
| Antioxidant and Oxygen-Control Measures | Limits oxidation of smoke-derived compounds and the food surface through oxygen control, suitable packaging, and legally permitted antioxidant systems. | Smoked meats, fish, nuts, snacks, ready-to-eat foods, and products with extended distribution cycles. | Residual oxygen, water activity, packaging oxygen transmission rate, light exposure, storage temperature, and shelf-life target. | Helps protect color, aroma, flavor, and lipid quality during storage and international transportation. | Does not replace proper smoke generation or application control; additive permissions vary by destination market. | Important for long-distance shipping, warm-climate distribution, and products with high unsaturated-fat content. |
| Barrier Packaging and Modified Atmosphere | Reduces oxygen, moisture, light, and aroma transfer after processing, helping retain smoke flavor and surface color. | Sliced meats, smoked fish, cheese, snack products, vacuum-packed foods, and chilled ready-to-eat products. | Oxygen transmission rate, water-vapor transmission rate, seal integrity, residual oxygen, gas composition, and package headspace. | Supports shelf-life management, reduces oxidation, and protects product quality during storage and distribution. | Packaging material selection must match product respiration, temperature, moisture, sealing equipment, and recycling requirements. | Highly relevant to global buyers because transport duration and climate conditions can vary significantly by market. |
| Digital Process Monitoring | Sensors and data logging track critical process variables, enabling corrective action before smoke flavor, color, or safety specifications drift. | All smoked products, especially high-volume production and facilities supplying multiple export markets. | Temperature, humidity, airflow, smoke density, product core temperature, exposure time, and batch records. | Improves traceability, repeatability, audit readiness, preventive control, and production efficiency. | Initial investment, sensor calibration, data integration, and staff training are required. | Recommended for international suppliers needing documented consistency and reliable quality records. |